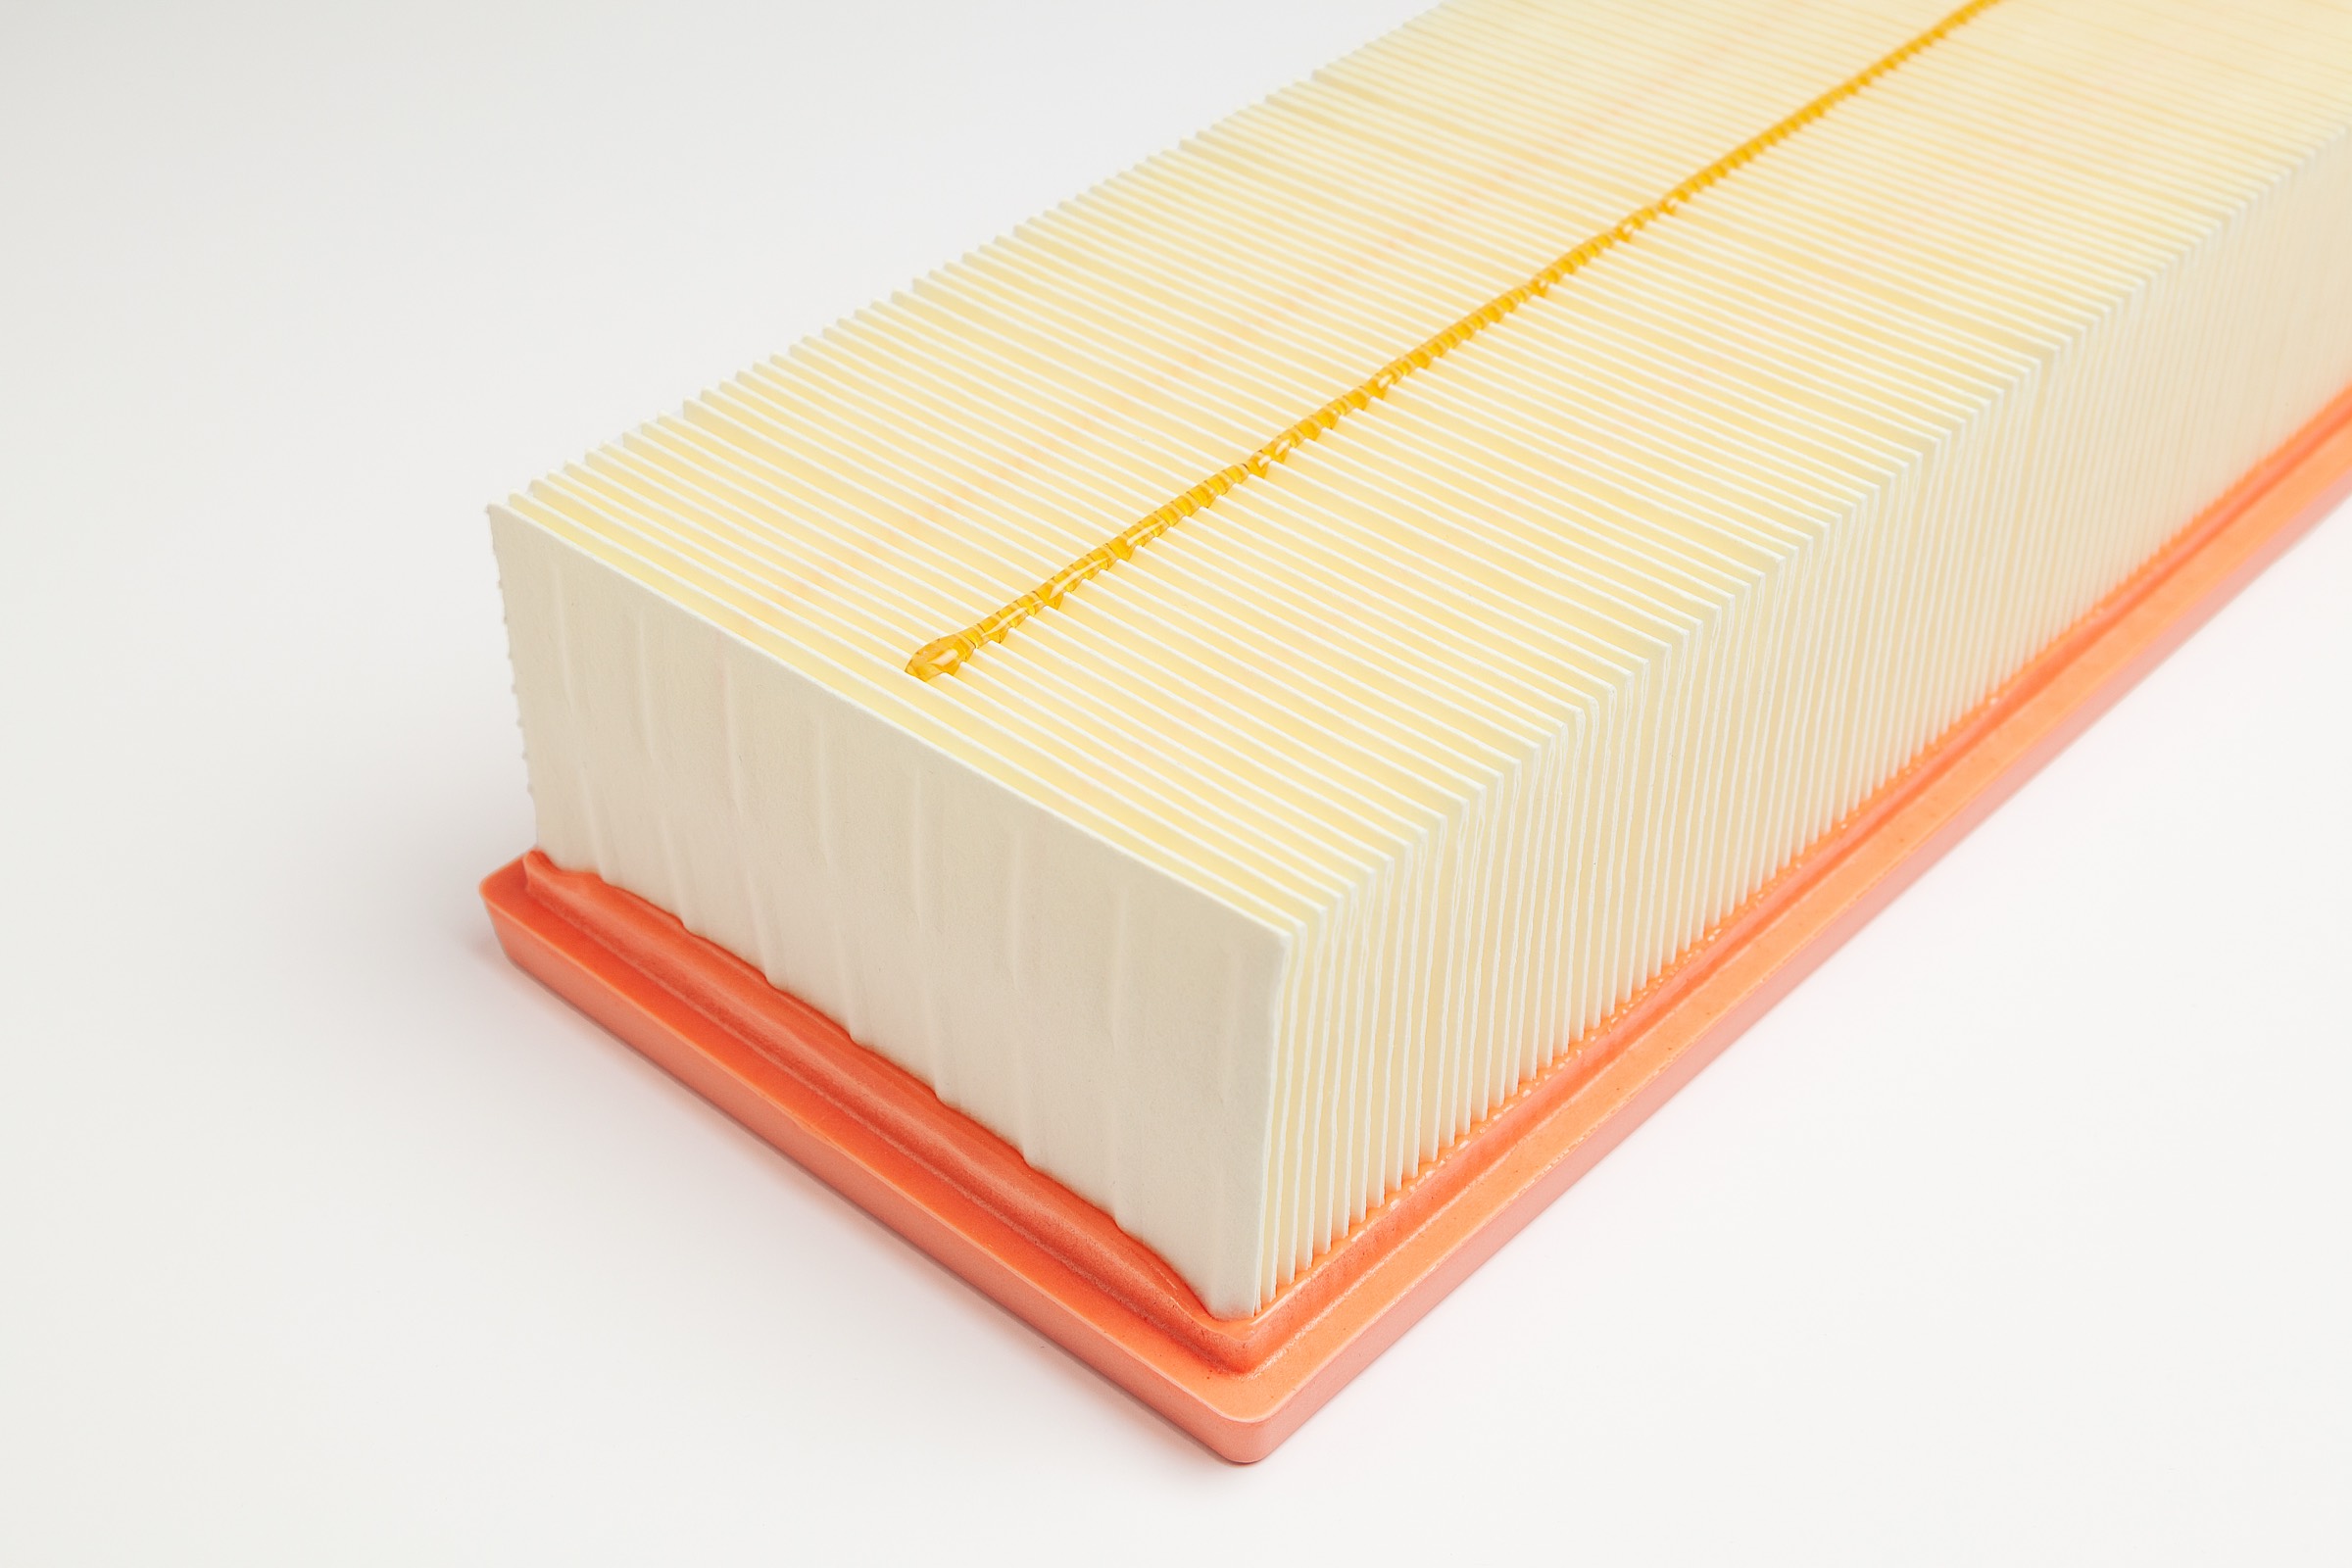
Technipol PA 2150
Copolyamide hot melt for engine air filters, 150 °C softening point, 7.5 Pa·s at 190 °C and Shore D 43. Rapid setting, 86 percent bio-based carbon.
Copolyamide hot melt for engine air filters, 150 °C softening point, 7.5 Pa·s at 190 °C and Shore D 43. Rapid setting, 86 percent bio-based carbon.
Technipol PA 2150 is a copolyamide hot-melt adhesive with a softening point of 150 °C, a Brookfield viscosity of 7.5 Pa·s at 190 °C and a Shore D hardness of 43. Sipol makes it for the production of engine air filters in the automotive sector.
Sipol describes a rapid setting time and an average application temperature, with good flexibility, wettability and chemical resistance. The melter profile puts the tank at 200 to 210 °C and the hose and nozzle at 210 to 220 °C.
The mechanical table puts numbers on that flexibility. Elongation at break is 285 percent, stress at break 9.5 MPa and flexural modulus 61 MPa, and hardness drops from 43 to 35 Shore D over 15 s under the indenter.
Sipol states more than 80 percent raw materials from non-edible renewable sources. The data sheet also carries a measured value, 86 percent bio-based carbon as a share of total carbon by ASTM D6866, the figure to quote in a carbon-content declaration.
It is also written as copolyamide hot melt adhesive, co-polyamide hot melt, polyamide hot melt adhesive, thermoplastic polyamide adhesive, and CoPA.
| Property | Typical value |
|---|---|
| Softening point | 150 °C (Sipol method MI 13) |
| Brookfield viscosity | 7.5 Pa·s at 190 °C (Sipol method MI 12, Brookfield CAP 2000+ cone and plate) |
| Density | 0.98 g/cm³ (ISO 1183) |
| Shore D hardness | 43 instantaneous, 35 after 15 s (ISO 868) |
| Elongation at break | 285 percent (ISO 527) |
| Stress at break | 9.5 MPa (ISO 527) |
| Flexural modulus | 61 MPa (ISO 178) |
| Renewable source content | 86 percent bio-based carbon of total carbon (ASTM D6866) |
| Renewable raw materials | More than 80 percent, from non-edible renewable sources (Sipol data sheet) |
| Form | Granules |
Typical values from the manufacturer's technical data sheet. They describe the product, they are not a specification. We will send the current TDS and the batch documentation your qualification needs.
Tell us the part or the process, the property you are targeting, and the volume you expect. We will confirm the grade, send the documentation, and get a sample of the candidate grade to you.
The use Sipol states for PA 2150 in the automotive sector.
Sipol's extrusion profile runs from 50 to 80 °C under the hopper to 190 to 210 °C at the nozzle.
Melter profile with the tank at 200 to 210 °C and the hose and nozzle at 210 to 220 °C.
Sipol's suggested extrusion profile: under the hopper 50 to 80 °C, feeding zone 110 to 140 °C, compression zone 150 to 170 °C, metering zone 180 to 200 °C, die or hose 180 to 200 °C, nozzle 190 to 210 °C.
Sipol's suggested melter profile: pre-heating grid 175 to 185 °C, tank 200 to 210 °C, hose 210 to 220 °C, nozzle 210 to 220 °C.
Both profiles are starting points. Equipment, bead size and line speed move the final settings.
Package sizes: 25 kg bags with an aluminum film moisture barrier, 500 kg cardboard octabins with an inner PE liner, and 500 kg big bags..
Storage: Stable for 24 months unopened in the original packaging, kept in a cool, dry place and protected from light. Material held at around 5 to 10 °C or below should stand at 15 to 20 °C for at least 24 hours before use.
Read the safety data sheet before handling.
Sipol makes Technipol PA 2150 for the production of engine air filters, and describes it as rapid setting with an average application temperature, good flexibility, good wettability and good chemical resistance. It softens at 150 °C and measures 7.5 Pa·s at 190 °C. The data sheet does not break the use down by operation, so confirm the bond, pleat or edge, in a trial on your own media.
Sipol's melter profile for Technipol PA 2150 runs the pre-heating grid at 175 to 185 °C, the tank at 200 to 210 °C and the hose and nozzle at 210 to 220 °C. The extrusion profile ends at 190 to 210 °C at the nozzle. The softening point is 150 °C, so the melt sits 50 to 70 °C above it at application. Treat both profiles as starting points.
Technipol PA 2150 carries a measured 86 percent bio-based carbon as a share of total carbon, by ASTM D6866, on Sipol's data sheet. Sipol separately states that more than 80 percent of its raw materials come from non-edible renewable sources. The ASTM D6866 value is the one to use where a customer asks for a tested carbon figure.
Technipol PA 2150 softens at 150 °C and is Shore D 43, with a 61 MPa flexural modulus and 285 percent elongation. Technipol PA 2188 softens at 188 °C and is Shore D 57, with a 198 MPa flexural modulus and 400 percent elongation, and its melter runs hotter, 230 to 240 °C at the nozzle. PA 2188's data sheet names oil filter pleat bonding and end caps as well as air filter work.
Yes. We send the Technical Data Sheet (TDS), Safety Data Sheet (SDS), and IMDS data on request, in the manufacturer's current revision. Use Request TDS or SDS above and tell us what your qualification review needs.
Lower-softening air filter grade at 131 °C for media that is not oven cured.
Automotive filter grade at 174 °C softening point and 4.0 Pa·s at 205 °C.
Harder 188 °C grade for edge sealing, pleat bonding and end caps.
The Technipol and Technipol PA range by softening point and use.
Air, oil and diesel filter bonding and the hot melts that do each job.
How to choose a hot melt for pleat, edge and end-cap bonding.